
Paper Packaging · Regulatory & Technical Insight
PPWR Is Now Applicable: How RT901 Supports the PFAS-Free Transition in Molded Fiber Packaging
The EU Packaging and Packaging Waste Regulation (PPWR) is changing how food-contact packaging manufacturers assess barrier chemistry. For molded fiber, the transition is not only about removing PFAS: it is about maintaining water and oil resistance, fitting the existing wet-end process and building a clearer finished-package validation framework.
Key takeaways
What does PPWR mean for molded fiber food packaging?
The EU Packaging and Packaging Waste Regulation (PPWR) applies from 12 August 2026, and its PFAS concentration limits for food-contact packaging also apply from that date. Other packaging requirements, including recyclability-related provisions, will be introduced progressively in later stages.
For molded fiber manufacturers serving food-contact applications, this creates both an immediate formulation challenge and a longer-term material-selection question. Barrier technology now needs to be considered together with finished-product performance, production practicality and compliance validation.
PFAS-free does not mean compromising barrier performance
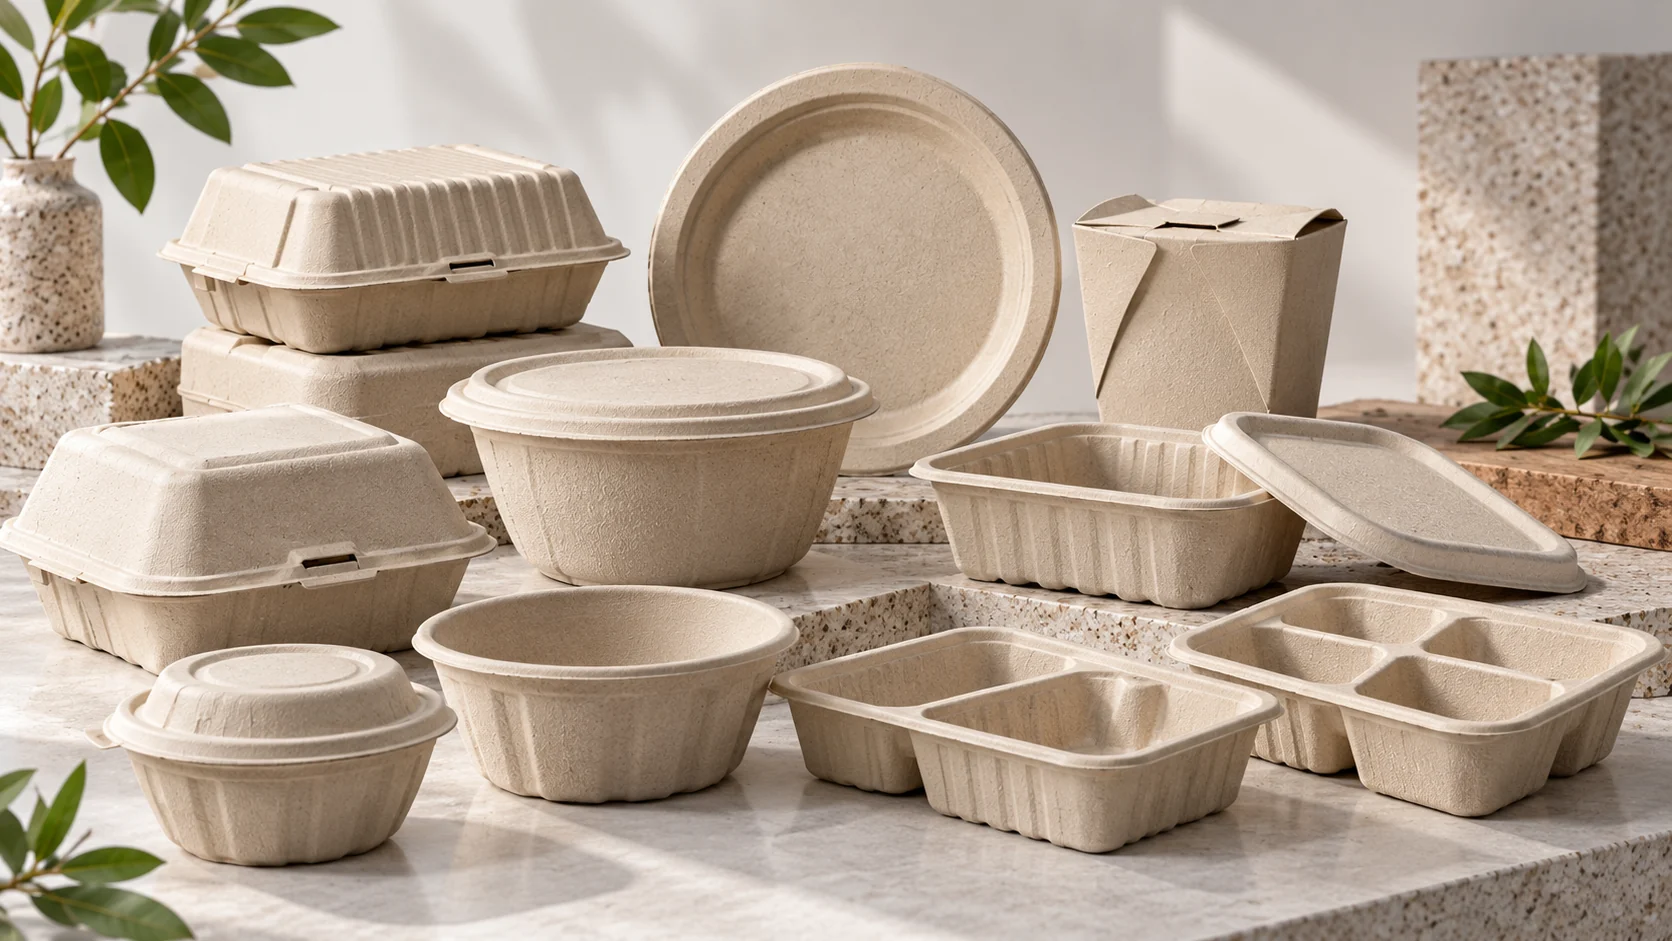
Molded fiber trays, plates, bowls, lids and takeaway containers still need to resist moisture, oil and grease under real use conditions. Fiber gives the package its structure, while the barrier system determines which temperatures, contact times and food conditions the product can handle.
RETERRA RT901 is a PFAS-free water- and oil-repellent additive developed for wet-end application in molded fiber production. It is designed to provide water and oil resistance across a 0–100°C application range. Under suitable formulation and molding conditions, molded fiber products treated with RT901 can achieve barrier performance against 100°C hot water and hot oil for at least 30 minutes.
Actual results depend on pulp type, dosage, forming conditions and finished-product design. Manufacturers should therefore validate performance using the final article and the target application standard.
Integrating barrier performance into existing wet-end production
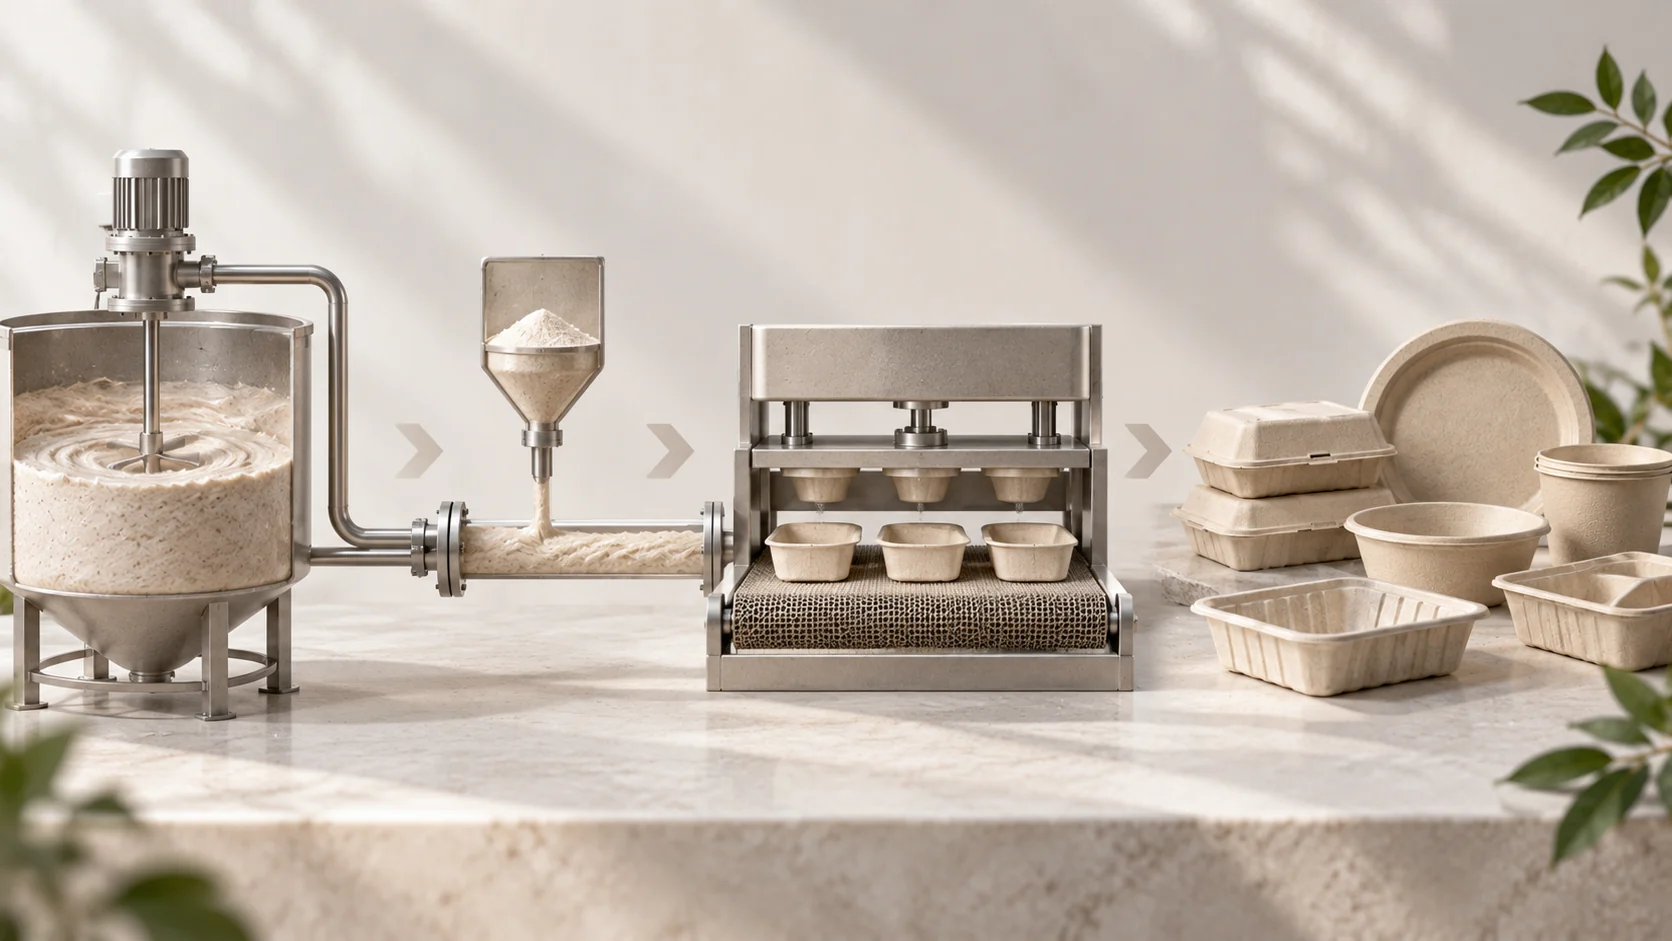
RT901 is introduced into the pulp slurry before forming, so the water- and oil-repellent function is built into the fiber system through the wet end. This allows manufacturers to work within the existing pulp preparation and molding workflow rather than creating a separate RT901 spraying or coating step.
For products with side walls, corners, grooves, compartments and other three-dimensional structures, wet-end addition provides a practical route for distributing barrier chemistry throughout the molded structure. Where application requirements can be met with RT901 alone, the same product can provide both water and oil resistance and reduce the need for separate water-repellent and oil-repellent additives.
Evaluating the total cost of PFAS-free barrier systems
The economics of PFAS-free conversion should not be assessed only by additive price per kilogram. A meaningful production comparison also includes actual dosage, supporting chemicals, equipment requirements, process steps, production efficiency, qualification rate and performance consistency across orders.
For industrial molded fiber applications, the typical recommended dosage of RT901 is 3.0–4.0% based on oven-dry pulp weight, with final dosage optimized according to pulp furnish, product design and target performance.
Building a clearer compliance validation framework under PPWR
The PPWR PFAS restrictions apply to the finished food-contact packaging. A PFAS-free barrier additive such as RT901 can support a PFAS-free formulation strategy, but complete verification should still consider the fiber furnish, other additives, process chemicals and any other potential sources of fluorinated substances in the manufacturing system.
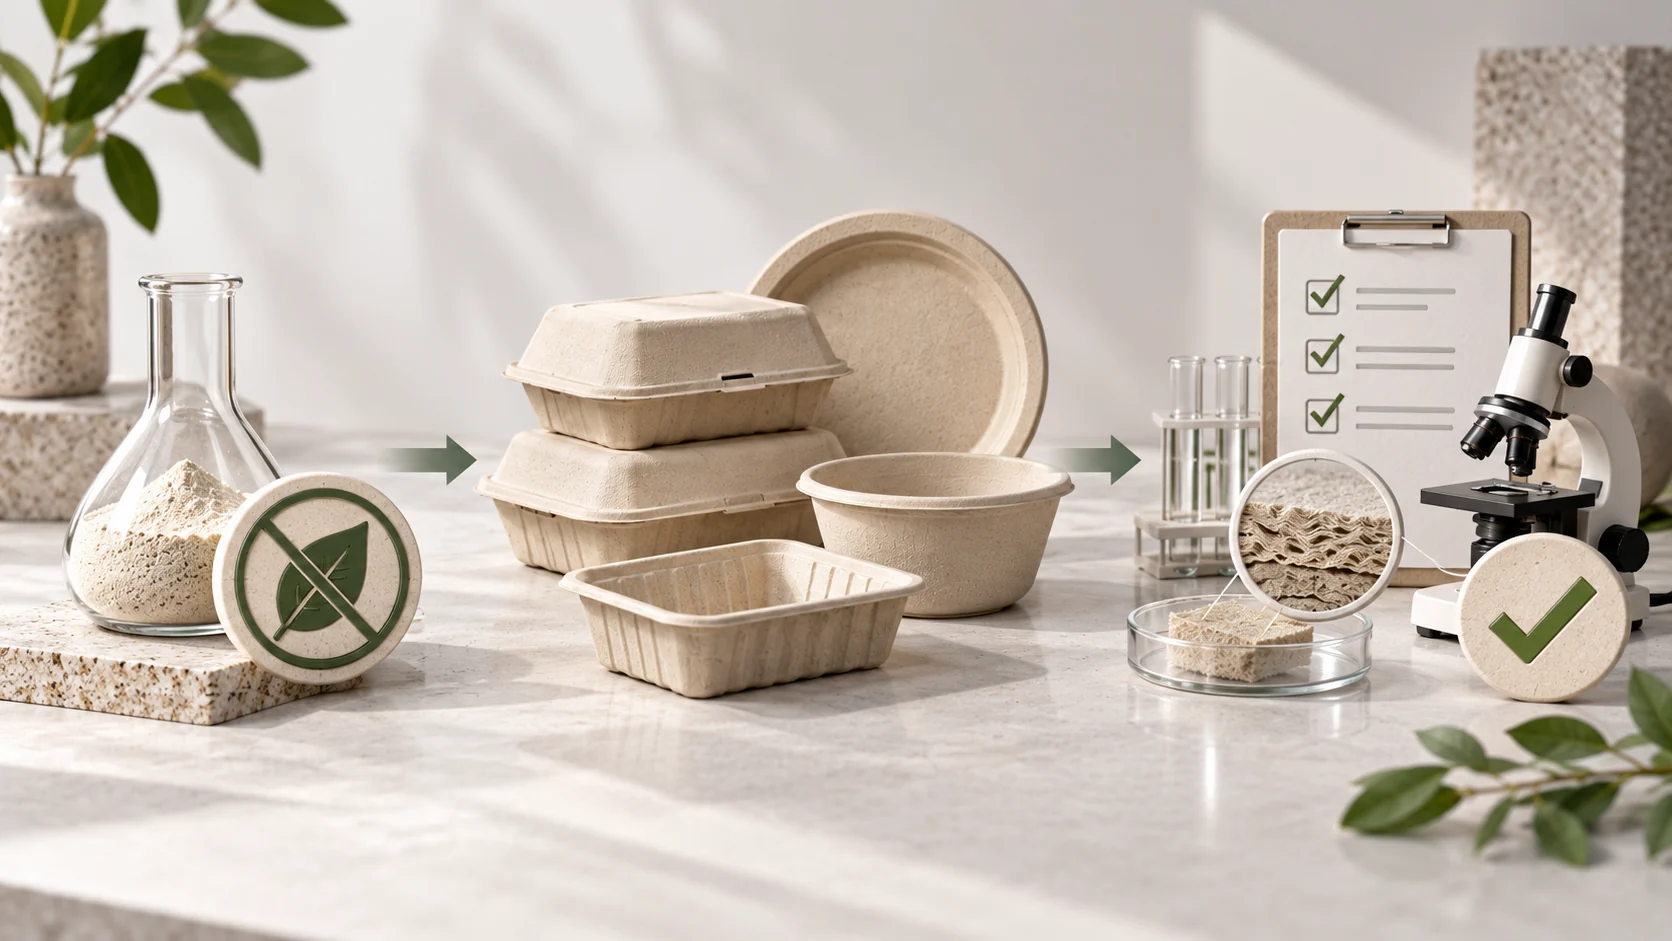
Manufacturers should validate the final packaging according to its intended use and applicable requirements. PFAS testing, food-contact compliance, recyclability and compostability are separate questions and should be assessed under the relevant rules and test methods for each claim.
RT901 gives manufacturers a defined basis for recording dosage, process conditions and finished-product performance. As regulatory requirements develop, traceable and repeatable validation records will become increasingly important in supplier qualification and customer procurement.
Preparing molded fiber packaging for the next stage of EU requirements
PPWR is encouraging packaging manufacturers to consider material selection, end-use performance and lifecycle requirements together. For molded fiber to expand into more demanding food-service applications, barrier technology must support practical production, reliable use performance and a defensible validation process.
RETERRA RT901 combines PFAS-free chemistry, water and oil repellency and wet-end application in a solution developed for molded fiber production. Its value is not simply the replacement of one chemistry with another, but the ability to develop a PFAS-free barrier system within an existing manufacturing process while keeping the focus on finished-package performance.
Frequently asked questions
What does PPWR mean for molded fiber food packaging?
For molded fiber food-contact packaging, PPWR means manufacturers need to consider PFAS limits, finished-package performance and future packaging requirements together. Material selection should therefore be supported by final-article testing and documented validation.
Does using a PFAS-free additive automatically make a package PPWR-compliant?
No. A PFAS-free additive supports a PFAS-free formulation strategy, but PPWR limits apply to the finished food-contact packaging. Fiber, other additives, processing chemicals and the final article still need to be assessed.
What is RT901 used for in molded fiber production?
RETERRA RT901 is a PFAS-free water- and oil-repellent additive designed for wet-end addition in molded fiber production. It is intended to help manufacturers develop barrier performance without adding a separate RT901 surface-coating step.
What dosage is typically used for RT901?
For industrial molded fiber applications, the typical recommended dosage is 3.0–4.0% based on oven-dry pulp weight. Final dosage should be optimized for the pulp furnish, product geometry, process conditions and target performance.
Can RT901 provide both water and oil resistance?
Yes, where the formulation and production conditions are suitable, RT901 can provide both water and oil repellency. Finished-product testing is still required to confirm performance for the intended use.